
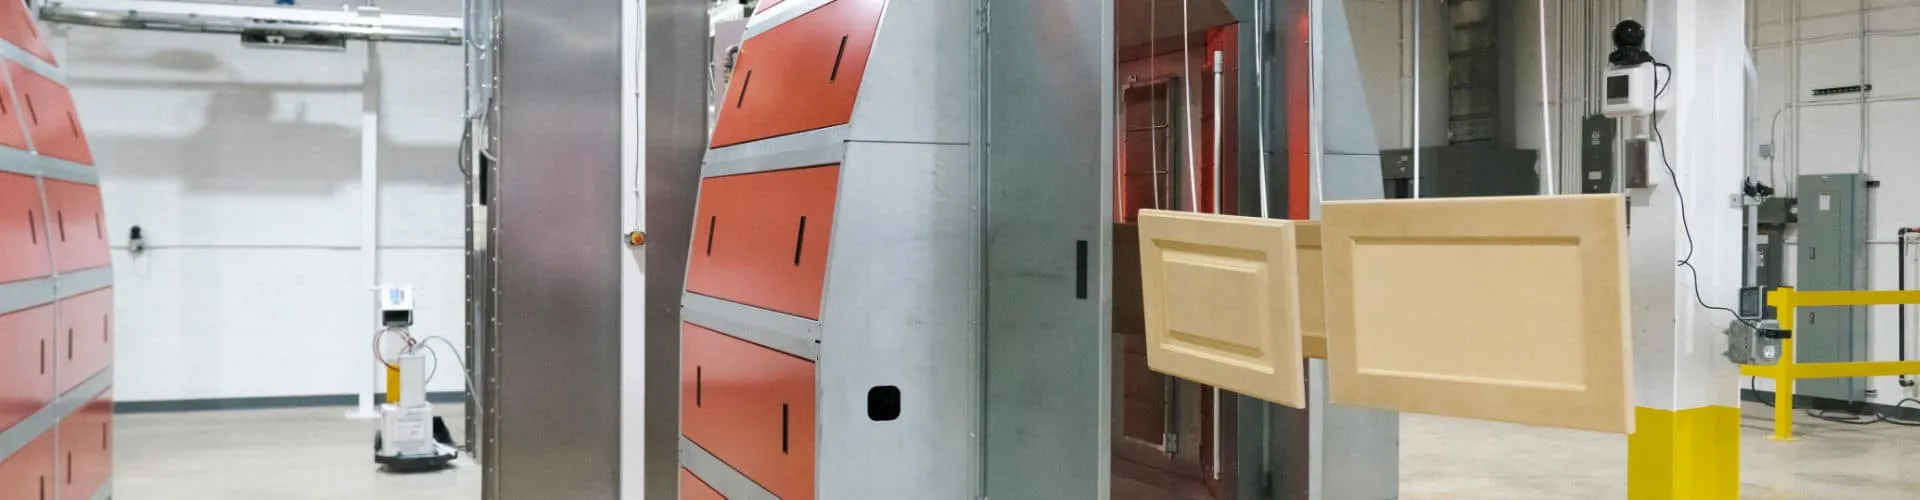
Engineered Wood Products
still painting engineered products? reduce handling with just 2 powder coats
MDF (Medium Density Fiberboard) dominates kitchen cabinetry, bathroom vanities, and furniture manufacturing due to its smooth surface, consistent quality, and cost-effectiveness. But moisture vulnerability—especially at cut edges—and multi-step liquid finishing processes create ongoing challenges for manufacturers. Painted or wrapped MDF edges often fail first, leading to warranty claims and customer dissatisfaction.
Powder coating MDF eliminates these headaches when done correctly. Gas Catalytic IR technology provides the precise, gentle heat profile needed to cure powder coating on heat-sensitive substrates without warping, outgassing defects, or edge failures. The result: sealed, moisture-resistant MDF panels with superior durability in single-cure workflows that eliminate VOC emissions and multi-coat complexity.
What’s more only two coats are required, a primer and final coat.
Liquid v. Powder on MDF
The MDF Challenge: Why Traditional Methods Fail
Why Convection Ovens Fail on MDF
Temperature Extremes:
Air temperatures of 350-400°F required for powder cure far exceed MDF’s safe operating range. Prolonged exposure (15-30 minutes typical) causes substrate degradation.
Uncontrolled Outgassing:
Cut MDF edges release moisture and volatiles when heated. In convection’s slow, uneven heating, these gases escape during the critical gel/flow stage, creating surface bubbles and porosity.
Warping and Distortion:
Extended exposure to high ambient temperatures causes MDF panels to warp, bow, or develop edge distortion. Thinner panels (12-18mm) are especially vulnerable.
Edge Failures:
Convection’s slow heat penetration fails to properly flow powder into and seal cut edges before substrate degradation begins.
Why Gas Catalytic IR Succeeds on MDF
Controlled, Gentle Heating:
IR energy heats powder coating and MDF surface directly without requiring extreme air temperatures. Peak substrate temperatures stay safely below 200°F while powder receives sufficient energy to cure completely.
Staged Outgassing Control:
Pre-heat stage (3-4 minutes at controlled temperature) allows gases to escape from cut edges before powder application and gel. This separates outgassing from the cure process.
Rapid Cure Minimizes Exposure:
Total heat exposure of 8-12 minutes—compared to convection’s 20-30 minutes—dramatically reduces risk of substrate damage while achieving complete cure.
Superior Edge Sealing:
Direct radiant energy flows powder into cut edges effectively, creating the sealed barrier critical for moisture resistance. Edge seal quality consistently exceeds 95%.
The Catalytic IR Process for MDF
Material Selection and Preparation
Substrate Selection:Use MDF grades designed for finishing—typically 680-780 kg/m³ density with low formaldehyde content.
Surface Preparation:Clean surfaces free of dust, oils, and contaminants. Light sanding (220-320 grit) improves powder adhesion.
Moisture Content:Verify MDF moisture content is 6-9% before coating. Higher moisture increases outgassing risk.
Pre-Heat Stage for Controlled Outgassing
Purpose:Controlled pre-heat (3-4 minutes at 220-250°F) brings MDF surface and edges to controlled temperature, allowing moisture and volatiles to escape before powder application.
Critical Benefits:
- Eliminates 90%+ of potential outgassing before cure
- Warms surface for improved powder attraction
- Identifies substrate issues before powder application
- Reduces edge bubbling to near zero
Powder Application
Timing:Apply powder immediately after pre-heat while substrate is still warm (improves attraction).
Parameters:Adjust voltage (60-90kV), powder flow, and gun distance for MDF geometry. Flat panels require different setup than profiled edges.
Edge Coverage:Use dedicated edge guns or multi-angle application to ensure complete edge coverage. This is where moisture protection succeeds or fails.
Film Build:Target 60-80 microns for optimal durability and edge sealing.
Gentle Cure with Galaxy Cure
Why Galaxy Cure:WolfRayet’s Galaxy Cure is specifically designed for heat-sensitive substrates requiring gentle, controlled cure profiles. Zone-by-zone control delivers precisely the energy needed without excess heat that damages MDF.
Cure Profile:
- Zone 1 (Gel):Bring powder to gel point (250-280°F powder temp)
- Zone 2 (Flow/Crosslink):Moderate heat as powder flows and crosslinks
- Zone 3 (Final Cure):Complete cure with peak MDF temp below 195-200°F
Total Time:8-12 minutes depending on powder type and panel thickness.
Common MDF Pitfalls and Solutions
Bubbles on Cut Edges
Cause: Outgassing not completed before powder gels
Solution
Poor Edge Coverage
Cause: Application parameters not optimized for edge geometry
Solution
Warping or Bowing
Cause: Cure profile too aggressive or total heat exposure too long
Solution
Inconsistent Results
Cause: Lack of process control and recipe management
Solution
Surface Roughness
Cause: Gel/flow temperature inconsistent or powder application issues
Solution
Frequently Asked Questions
Can I run MDF and metal parts on the same powder coating line?
Yes, with proper planning. Metal parts typically require higher cure temperatures and different dwell times than MDF. The solution: Use Galaxy Cure’s PLC recipe management to store and quickly switch between substrate-specific profiles. Line scheduling can batch MDF runs together, then switch to metal profiles. Changeover takes 1-2 minutes.
Do I need separate equipment for MDF powder coating?
Not necessarily. A well-designed catalytic IR system like Galaxy Cure can handle both metal and MDF substrates with different cure profiles. The critical requirements: PLC-controlled zone management, pre-heat capability, and gentle heat profiles. Existing metal powder coating lines can often be adapted or upgraded for MDF capability.
What about formaldehyde emissions from MDF?
Modern low-formaldehyde and CARB2-compliant MDF grades minimize this concern. The pre-heat stage allows any residual off-gassing before powder application. Properly cured powder coating also acts as a barrier reducing any long-term emissions from the substrate.
How does powder coating compare to thermofoil wrapping?
Powder coating provides superior edge sealing and moisture resistance compared to wrapped MDF. Wrapped edges remain a weak point prone to delamination in high-moisture environments. Powder coating creates a seamless, sealed finish including edges. However, powder coating has aesthetic limitations (solid colors, no wood grain) compared to thermofoil’s decorative options.